OEM Econom Press Brake: What to Look for Before You Buy
2026-09-30
Most shops shopping for an OEM economy press brake start with the wrong question: 'What can I get for the least money?' The smarter question is 'What will this machine still do well five years from now?' That shift in focus changes everything. You stop chasing the lowest quote and start looking at frame construction, control repeatability, and the manufacturer's track record—things HUNSONE treats as non-negotiables. In this guide, we'll walk through the checks that separate a genuine bargain from an expensive mistake.
Start With the Frame, Not the Flashy Specs
Most people shop for a bike like they're buying a spec sheet on wheels: how many gears, how light, how much travel. But that's like picking a house based on its doorknobs. The frame is the soul of the ride—its geometry, the way it flexes under load, the subtle curve of the stays that decides whether you feel planted or twitchy at speed. Without a frame that fits your body and your intentions, no carbon wheel or electronic shifter will save you from a bike that fights you on every climb.
A well-chosen frame disappears beneath you. It translates your pedal strokes into forward motion without drama, holds a line through loose corners, and lets you forget the machine entirely. Flashy components, on the other hand, can be swapped later—a new groupset, lighter wheels, a dropper post. The frame is the one thing you can't easily change, and it dictates how every upgrade will feel. Beg, borrow, or test-ride as many frames as you can before committing. Your lower back and your descending confidence will thank you.
Think of it this way: a cheap frame with expensive parts is still a cheap ride, but a great frame with modest parts is a bike you'll keep for a decade. The shine of a carbon crank fades; the dull thud of an aluminum frame that doesn't fit never does. Start with the foundation—the angles, the wheelbase, the standover—and build from there. Specs are seductive, but the frame is the truth.
Tonnage You Can Calculate Without a Sales Rep
Figuring out the right cooling capacity for your space doesn’t require a phone call or a site visit. Start with the square footage of the area you want to cool. A widely used baseline is about one ton of cooling per 400 to 600 square feet, depending on your climate, insulation, and sun exposure. So a 1,500-square-foot home in a moderate climate often lands around 2.5 to 3 tons. That alone can give you a working number before anyone tries to upsell you.
If you want a more precise estimate, you can dig into the details yourself. Measure ceiling height, count large windows, and note how many people typically occupy the room. Add about 600 BTU per person and another 1,000 BTU per window that gets direct afternoon sun. Then divide the total BTUs by 12,000 to get tons. For example, a 20-by-20 room with two people and one sunny window might need roughly 8,000 to 9,000 BTU, or about 0.7 to 0.75 tons. It’s not a replacement for a full load calculation, but it puts you in control.
The real advantage is having a baseline before you talk to any contractor. When someone quotes you a 4-ton unit for a space you measured at 2.5 tons, you’ll know to ask why. Write down your square footage, window count, and insulation type, then do the math yourself. It takes ten minutes and saves you from accepting a number you can’t verify.
Controls That Don't Fight You on Every Bend
The steering wheel settles into your hands with a weight that feels deliberate, not heavy. Through a long sweeper, there's no need to saw at the rim or make endless micro-corrections. The car tracks its line with an almost intuitive calm, letting you focus on the road instead of wrestling the front end.
Even when the surface gets patchy or camber changes mid-corner, the feedback stays clear without turning abrupt. You get just enough information through the wheel to know what the tires are doing, but not so much that every ripple becomes a tug-of-war. That balance is what makes hour-long drives feel less like work and more like a rhythm.
What stands out most is the lack of constant adjustment. The system doesn't overcorrect or add artificial stiffness just to feel sporty. It simply reads your input and responds in kind, so the car goes where you point it without demanding constant vigilance. That's the kind of control that fades into the background and lets the drive itself take over.
Backgauge Repeatability Is the Real Accuracy Story
When a press brake operator talks about accuracy, they rarely mean the absolute position readout on the controller. What actually determines whether a batch of parts comes out consistent is how closely the backgauge returns to the same spot, bend after bend. That repeatability, not the nominal positioning precision, is what separates dependable production from constant fiddling.
Consider a machine whose backgauge can position itself to a displayed value of 100.00 mm with stunning resolution, yet every time it moves away and comes back, it lands at 99.98, then 100.03, then 99.97. Those tiny shifts translate directly into uneven flange lengths and inconsistent bend angles across the run. A backgauge with slightly less resolution but rock-solid return performance will beat it every time, because the operator can simply offset the program once and trust every part to match.
On the shop floor, repeatability shows up as fewer rejects, less time spent measuring and adjusting, and the confidence to run lights-out or with minimal oversight. Modern CNC press brakes advertise backgauge repeatability in the range of plus or minus 0.01 mm, and that figure carries far more weight than any single-axis positioning spec. It is the quiet metric that keeps a whole production schedule on track.
Tooling Compatibility You Won't Have to Re-Buy
Most workshops already have a drawer full of precisely chosen tools that earn their keep every week. The last thing anyone wants is a new machine that treats those tools as obsolete. Here, the connection points follow long-standing conventions rather than a proprietary twist, so the collets, bases, and guides you already own continue to work without a single adapter plate.
That same logic extends to software and calibration. If your current CNC controller or spindle drive talks over a standard pulse interface, it plugs right in—no forced firmware swap, no licensed dongle. The hardware reads the same g-code dialects and tool-length offsets you’ve been using, which means the learning curve is measured in minutes, not weekends.
What really saves money isn’t just avoiding a one-time accessory purchase; it’s the ongoing freedom to buy once and use everywhere. When a part wears out, you can source a replacement from a local supplier or an online marketplace instead of waiting on a single vendor’s backorder. That kind of compatibility is less about clever marketing and more about respecting the tools people already trust.
Support After the Invoice Is Paid
Once payment clears, our involvement actually becomes more hands-on. You can reach the same people who configured your setup directly. There's no queue handoff or need to re-explain your goals every time a question comes up.
We schedule a thirty-day check-in as a default, not as an upsell. It's a chance to review what's working, adjust any settings that feel off, and catch small issues before they turn into larger problems. Most of these calls end with a short list of tweaks we implement the same week.
Beyond that, you'll hear from us when something relevant changes—new features, deprecations, or shifts in best practices that affect your use case. You won't get a weekly newsletter. You'll get a note when it actually matters.
FAQ
The Econom line focuses on structural rigidity and simplified hydraulics rather than packing in features you may never use. You get a heavier frame and fewer electronic frills, which matters more for repeatable bends than a long spec sheet.
Look for a monolithic welded frame with stress-relieved construction. Avoid bolted-together side panels. A one-piece frame resists deflection under full tonnage, so the ram stays parallel even during off-center loads.
A controller with angle correction, backgauge memory, and fast manual jog modes will save more time than a touchscreen with hundreds of presets. Make sure you can store at least 50 programs and adjust sequences without a laptop.
Tonnage only tells you how thick a sheet you can bend. The backgauge determines how precisely you can locate each bend. A rigid backgauge with ball screws and a servo drive gives repeatable positioning, while a flimsy chain-driven gauge drifts after a few cycles.
Standard European-style punches and dies with a manual or pneumatic clamping system keep changeovers under five minutes. Avoid proprietary tooling that locks you into one supplier, and check whether the ram has a quick-release slot for sectional tooling.
Ask for a documented test report showing the cylinder holding pressure for at least 30 minutes without drift. On-site, run the ram to full tonnage and watch the pressure gauge and hose fittings. Any drop below 5 percent or visible weeping means the seals or valves were not properly lapped.
You want a distributor or factory office that can send a technician within 48 hours, not a reseller who only forwards emails. Ask for the nearest service hub, spare parts inventory for seals and valves, and whether they offer remote diagnostics via a standard internet connection.
Yes, often in rigging, leveling, and electrical hookup. Confirm whether the price includes unloading, anchoring, and a startup visit. Some sellers quote only the machine, then charge extra for commissioning and operator training, which can add five to ten percent to your total.
Conclusion
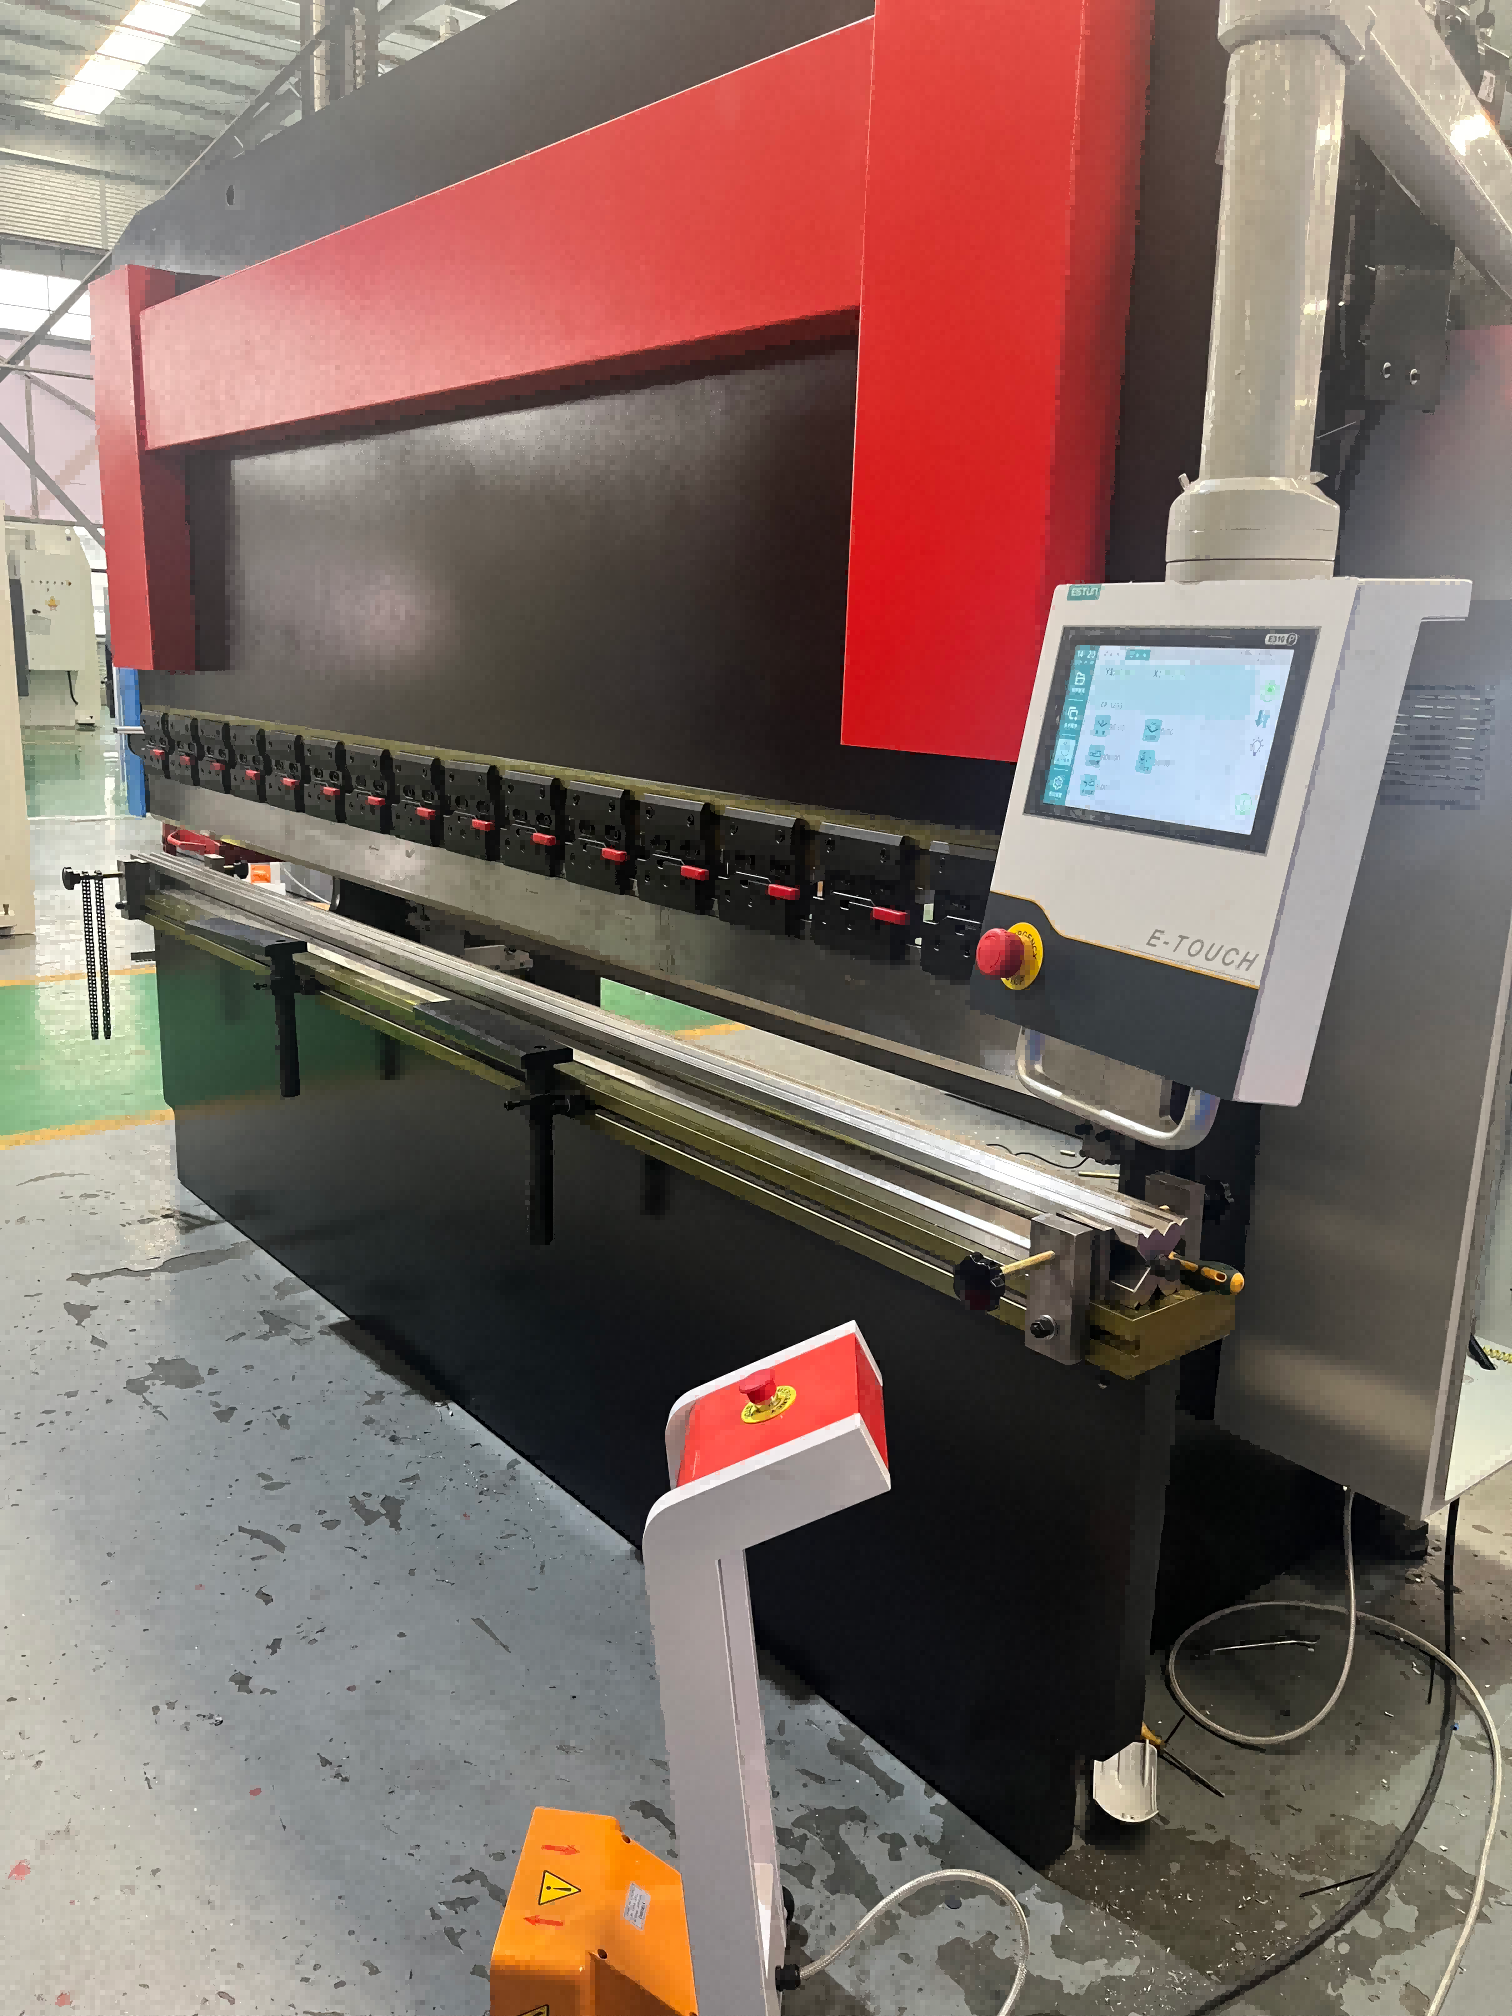
Start by examining the frame and overall build quality rather than chasing impressive specification sheets. A rigid, well-welded frame reduces deflection under load, which directly affects bending accuracy over time. You can estimate the required tonnage yourself using standard formulas based on material thickness, bend length, and die opening—no need to rely on a salesperson's recommendation. Once you've narrowed down capacity, spend time with the control system. If the interface requires extra steps for simple angle corrections or forces you to memorize nested menus, daily production will suffer. Good controls should let you adjust bend angles, set backgauge positions, and store common jobs with minimal friction.
The backgauge's repeatability matters more than the machine's advertised positioning accuracy. A backgauge that returns to the same spot bend after bend, even after thousands of cycles, keeps parts consistent without constant manual checks. Also look at tooling compatibility—standard clamping and common punch and die sizes mean you can use existing tooling or buy affordable replacements instead of being locked into proprietary systems. Finally, ask how support is handled after the invoice is paid. Response time for trouble-shooting, access to spare parts, and availability of local service technicians will determine whether a minor issue turns into days of downtime. A press brake is a long-term investment, so the relationship behind the machine matters just as much as the steel in front of you.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/