China INNOMOTICS High Voltage Motors Factory Sets New Standards in Industrial Drive Technology
2026-09-13
The hum of a high-voltage motor has long been the heartbeat of heavy industry, but lately, that heartbeat is getting stronger, quieter, and far more precise. At China's INNOMOTICS High Voltage Motors Factory, a quiet revolution is underway—one that challenges long-held assumptions about power density, efficiency, and reliability. As the facility pushes industrial drive technology into new territory, industry observers, including the team at Chuangjuman, are paying close attention. Because when standards shift this dramatically, the ripple effects are felt far beyond the factory floor.
Raising the Bar for High-Voltage Motor Efficiency
High-voltage motors have long been the workhorses of heavy industry, quietly consuming massive amounts of energy while receiving far less scrutiny than their low-voltage counterparts. The push to raise the bar for their efficiency isn't just a matter of regulatory compliance—it's a fundamental rethinking of how these machines are designed, built, and operated in real-world conditions. Traditional efficiency standards often rely on idealized lab tests that fail to capture the messy reality of fluctuating loads, harmonic distortion, and thermal cycling. A growing number of engineers and plant operators are demanding a more honest accounting, one that measures performance across the entire duty cycle rather than a single operating point.
The technical levers for improvement are surprisingly varied. Winding design has moved beyond simple copper-versus-aluminum debates into the realm of custom slot geometries and advanced insulation materials that allow for tighter packing and reduced I²R losses. Rotor construction is being revisited too, with die-cast copper rotors finally overcoming their manufacturing hurdles to deliver lower slip and higher conductivity. Meanwhile, the integration of variable frequency drives—once seen as add-ons—is now being treated as a core design parameter, enabling motors to adapt their magnetic flux in real time. These aren't incremental tweaks; they represent a shift in how motor manufacturers think about the interplay between electrical, mechanical, and thermal stresses.
Yet raising the bar isn't solely about hardware. The most forward-thinking facilities are pairing better motors with smarter monitoring, using embedded sensors and cloud-based analytics to track efficiency drift over years of service. This matters because even the best-designed motor will lose performance if bearings wear unevenly or cooling passages clog with dust. By treating efficiency as a dynamic property rather than a nameplate rating, operators can schedule maintenance before losses compound. The result is a quieter revolution—one where high-voltage motors stop being invisible energy sinks and start acting as intelligent partners in the push toward more sustainable industrial operations.
Inside INNOMOTICS' Precision Manufacturing Hub in China
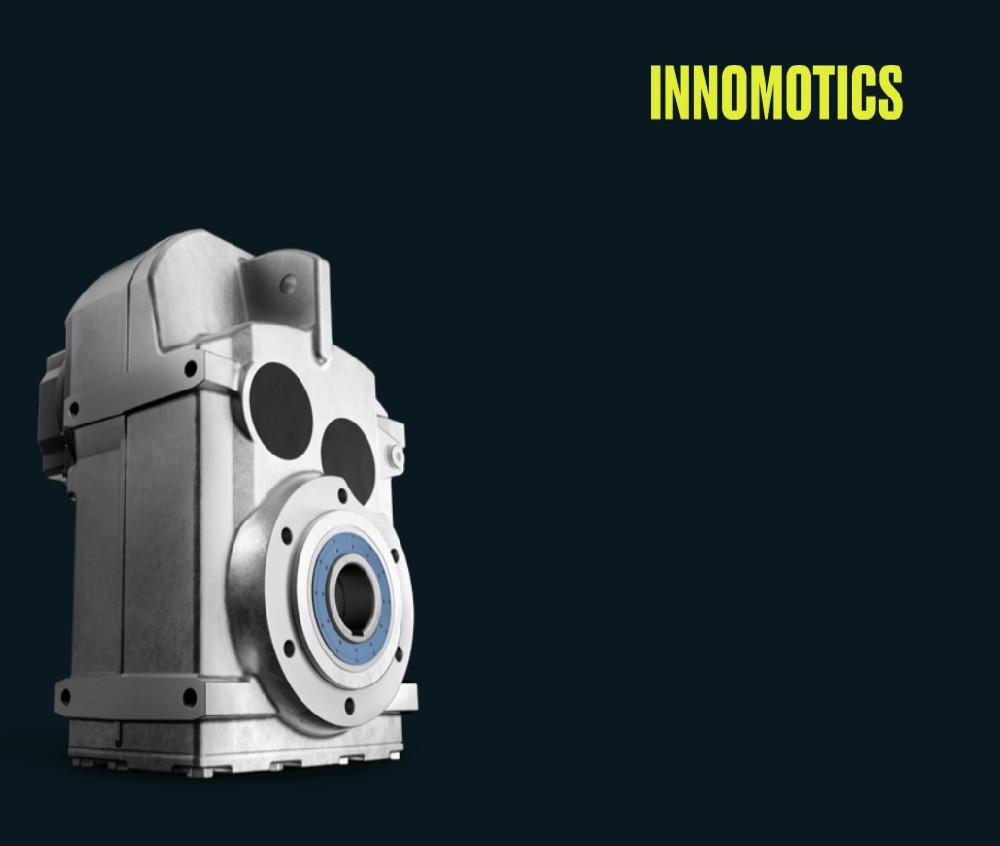
Step past the glass doors of INNOMOTICS' facility in Nanjing and the first thing you notice is the quiet. Not silence, but a low, purposeful hum that comes from rows of CNC machines turning aluminum and steel with micron-level patience. This isn't a place where parts are merely assembled; it's where the company's obsession with motion control takes physical form. Every surface, every calibration jig, every technician's measured movement speaks to a simple idea: if a motor is going to spin quietly inside a hospital ventilator or hold steady in a robotic arm, it has to be born from an environment that treats tolerance as a moral value.
Walk deeper and the scale reveals itself. A single hall houses the entire journey—from raw alloy billets sliding into automated lathes to finished servo motors undergoing 48-hour endurance tests in glass-walled chambers. What sets this hub apart isn't the machinery alone, though the five-axis grinders and laser interferometers are impressive. It's the way engineers here refuse to separate design from manufacture. A young team huddles around a prototype stator, not with laptops but with calipers and a whiteboard covered in hand-drawn flux diagrams. One of them notices a slight asymmetry in the winding pattern—something a CAD model wouldn't flag—and within minutes the production line adjusts. That loop, from idea to correction in the time it takes to finish a coffee, is the real reason this floor feels alive.
And then there's the testing pit, an unglamorous corner where motors are bolted to dynamometers and pushed past their rated loads until they fail. Failures are logged, dissected, and turned into next-week design changes. It's the opposite of marketing gloss: here, a scraped bearing race or a burned winding is evidence of a process that respects physics over promises. For anyone who's ever wondered why a German-engineered actuator costs more than a generic one, this room is the answer. The equipment doesn't just measure output; it measures doubt—and then systematically removes it.
Advanced Thermal Management for Continuous Heavy-Duty Operation
Keeping a heavy-duty engine cool under uninterrupted load is far more than just adding a bigger radiator. The core challenge lies in managing heat rejection from multiple sources simultaneously—combustion chambers, turbocharger housings, transmission oil coolers, and even the alternator under sustained high output. A well-designed thermal management system uses staged cooling circuits that prioritize cylinder head temperature control before routing coolant to less critical components, preventing localized boiling and thermal fatigue. This approach becomes especially critical when ambient temperatures exceed 45°C and the engine never stops running.
Modern solutions incorporate electronically controlled viscous fan clutches and variable-speed water pumps that respond to real-time coolant temperature sensors rather than simple belt-driven constant speeds. By decoupling cooling effort from engine RPM, the system can maintain optimal coolant flow during low-speed, high-load scenarios like uphill hauling with a full payload. Additionally, using low-silicate organic acid technology (OAT) coolants with higher boiling points and better heat transfer coefficients reduces the risk of vapor lock in the cylinder head, a common failure point in continuous duty cycles.
Field data from mining and long-haul trucking operations shows that implementing predictive thermal modeling can extend major overhaul intervals by up to 20%. Instead of reacting to overheating alarms, operators can monitor trends in coolant temperature delta across the radiator, oil temperature rise rates, and exhaust gas temperature (EGT) to anticipate degradation before it occurs. This proactive stance, combined with periodic cleaning of charge air coolers and radiator fins in high-dust environments, ensures that the thermal management system never becomes the bottleneck for productivity.
Customized HV Drive Solutions for Mining, Cement, and Power
Mining operations demand drives that cope with extreme dust, vibration, and altitude. Our HV drive systems are built around the specific duty cycles of conveyors, mills, and hoists, with thermal management tuned for underground heat and harmonic filtering matched to weak grid conditions. Rather than forcing a standard cabinet into a tough site, we adapt the enclosure, cooling path, and control logic to the actual ore body and production schedule.
Cement plants face frequent starts, high inertia loads, and abrasive environments. We configure medium-voltage drives for kiln ID fans, raw mills, and crushers using tailored overload curves and flux optimization that reduce mechanical stress during acceleration. The result is fewer trips, longer bearing life, and a lower energy bill, without relying on one-size-fits-all parameter sets.
Power generation and auxiliary systems require drives that stay online during grid disturbances. Our customized HV solutions include ride-through options, fast-acting protection, and redundancy plans for boiler feed pumps, draft fans, and condensate systems. Each drive is engineered around the plant's fault tolerance targets and maintenance windows, so a single specification sheet never dictates the design.
Automated Testing and Quality Control at Every Production Stage
Quality control at every production stage isn't a final checkpoint—it's a rhythm that runs through the entire build. Instead of waiting for defects to surface at the end, teams embed automated checks directly into each phase: from the first line of code to the final packaging run. A unit test fails the moment a function breaks; a visual regression flags a misaligned button before it reaches staging; a hardware-in-the-loop script catches a sensor drift while the assembly line is still moving. This early detection turns quality into a byproduct of the process rather than a costly afterthought.
The real advantage shows up in how quickly feedback reaches the people who need it. When a machine vision system inspects a part and immediately logs a dimensional deviation, the operator can adjust the tooling before the next cycle—not after a batch of rejects piles up. Similarly, a CI pipeline that runs static analysis, security scans, and integration tests on every commit gives developers a precise map of what broke and why, often within minutes. That tight loop between doing the work and validating it keeps small issues from compounding into release-blocking failures.
What makes this approach stick is that testing becomes part of the definition of done for each stage, not a separate gate bolted on at the end. A printed circuit board isn't considered assembled until the automated optical inspection passes; a firmware build isn't ready for merge until the power-consumption tests run clean; a production batch isn't shipped until the end-of-line functional test records its traceability data. By treating quality as a condition for moving forward—stage by stage—teams stop firefighting defects after the fact and start preventing them where they're born.
Digital Integration and Predictive Maintenance for Modern Drives
Digital integration in modern drives goes beyond connecting devices to a network. It involves harmonizing data flows between variable frequency drives, PLCs, sensors, and cloud or edge platforms so operational context travels with every torque and speed reading. When integration is done well, a drive stops being an isolated actuator and becomes a source of actionable insight.
Predictive maintenance adds the time dimension. Instead of replacing bearings or capacitors on a fixed schedule, algorithms look at subtle shifts in current signature, thermal behavior, and vibration patterns. A slight increase in motor current at a specific frequency can indicate bearing wear weeks before audible noise appears. This allows maintenance teams to plan work during scheduled downtime rather than reacting to an unplanned stop.
The real payoff appears when digital integration and predictive maintenance work together. Maintenance histories, load profiles, and real-time telemetry stay in one accessible environment, so the drive's condition is always understood in context. Teams can compare similar drives across plants, spot abnormal deviations early, and prioritize interventions where they matter most. It's a shift from routine checklists to evidence-based decisions that extend equipment life and reduce energy waste.
FAQ
The facility integrates automated winding and robotic varnishing lines with real-time vibration and temperature monitoring on every motor, so quality data is captured from the first coil to final test instead of being checked only at the end.
It pairs high-efficiency motor designs with digital twin simulations during production, letting engineers spot thermal or mechanical stress points before a unit is assembled, which shortens commissioning and extends service life.
Heavy sectors like mining, cement, steel, and large-scale water treatment gain the most, because the high voltage motors are built to handle continuous duty cycles with lower temperature rise and tighter vibration limits.
Beyond IEC and GB compliance, the plant adopted ISO 50001 energy management and uses its own stricter internal test protocols for partial discharge and bearing insulation, so motors often exceed the baseline requirements.
Yes, domestic manufacturing cuts lead times by several weeks compared with importing, and the site keeps a shared spare parts hub plus local field engineers who can respond to commissioning or retrofit requests without long international coordination.
Efficiency is treated as a production parameter, not just a design goal; each motor's losses are measured under load, and the data feeds back into stator and rotor adjustments to consistently hit IE4 or IE5 equivalent performance.
It uses vacuum pressure impregnation for winding insulation and runs a 72-hour endurance test for select motor frames under simulated overload and voltage fluctuation, which helps catch insulation weaknesses that normal factory tests miss.
It signals a shift from volume-focused output to precision manufacturing with embedded diagnostics, making high voltage motors smarter and easier to maintain while lowering total cost of ownership for plant operators.
Conclusion
China's INNOMOTICS high voltage motors factory has redefined what industrial drive technology can achieve, pushing efficiency benchmarks to levels that were once considered impractical. The facility's engineering teams have focused on raising the bar for high-voltage motor efficiency through optimized electromagnetic designs and low-loss core materials, while advanced thermal management systems ensure continuous heavy-duty operation without derating even in demanding mining and cement environments. Inside the precision manufacturing hub, automated production lines and rigorous testing at every stage—from stator winding to final assembly—guarantee consistent quality, with digital integration enabling real-time monitoring and predictive maintenance that reduces unplanned downtime for power plants and large-scale industrial users.
Rather than offering off-the-shelf products, the factory excels at customized high-voltage drive solutions tailored to specific operational profiles, whether it's a conveyor drive in a remote mine or a fan application in a cement kiln. The combination of precision manufacturing, automated quality control, and embedded digital diagnostics positions INNOMOTICS' Chinese facility as a benchmark for modern drive production, setting new standards in reliability, energy savings, and total cost of ownership that competitors are now scrambling to match.
Contact Us
Contact Person: Jony
Email: [email protected]
Tel/WhatsApp: 086-0571-86161808
Website: https://en.hzcjm.com/